Recloser Factory Production Lines and Advanced Testing for Grid Resilience
2026-10-04
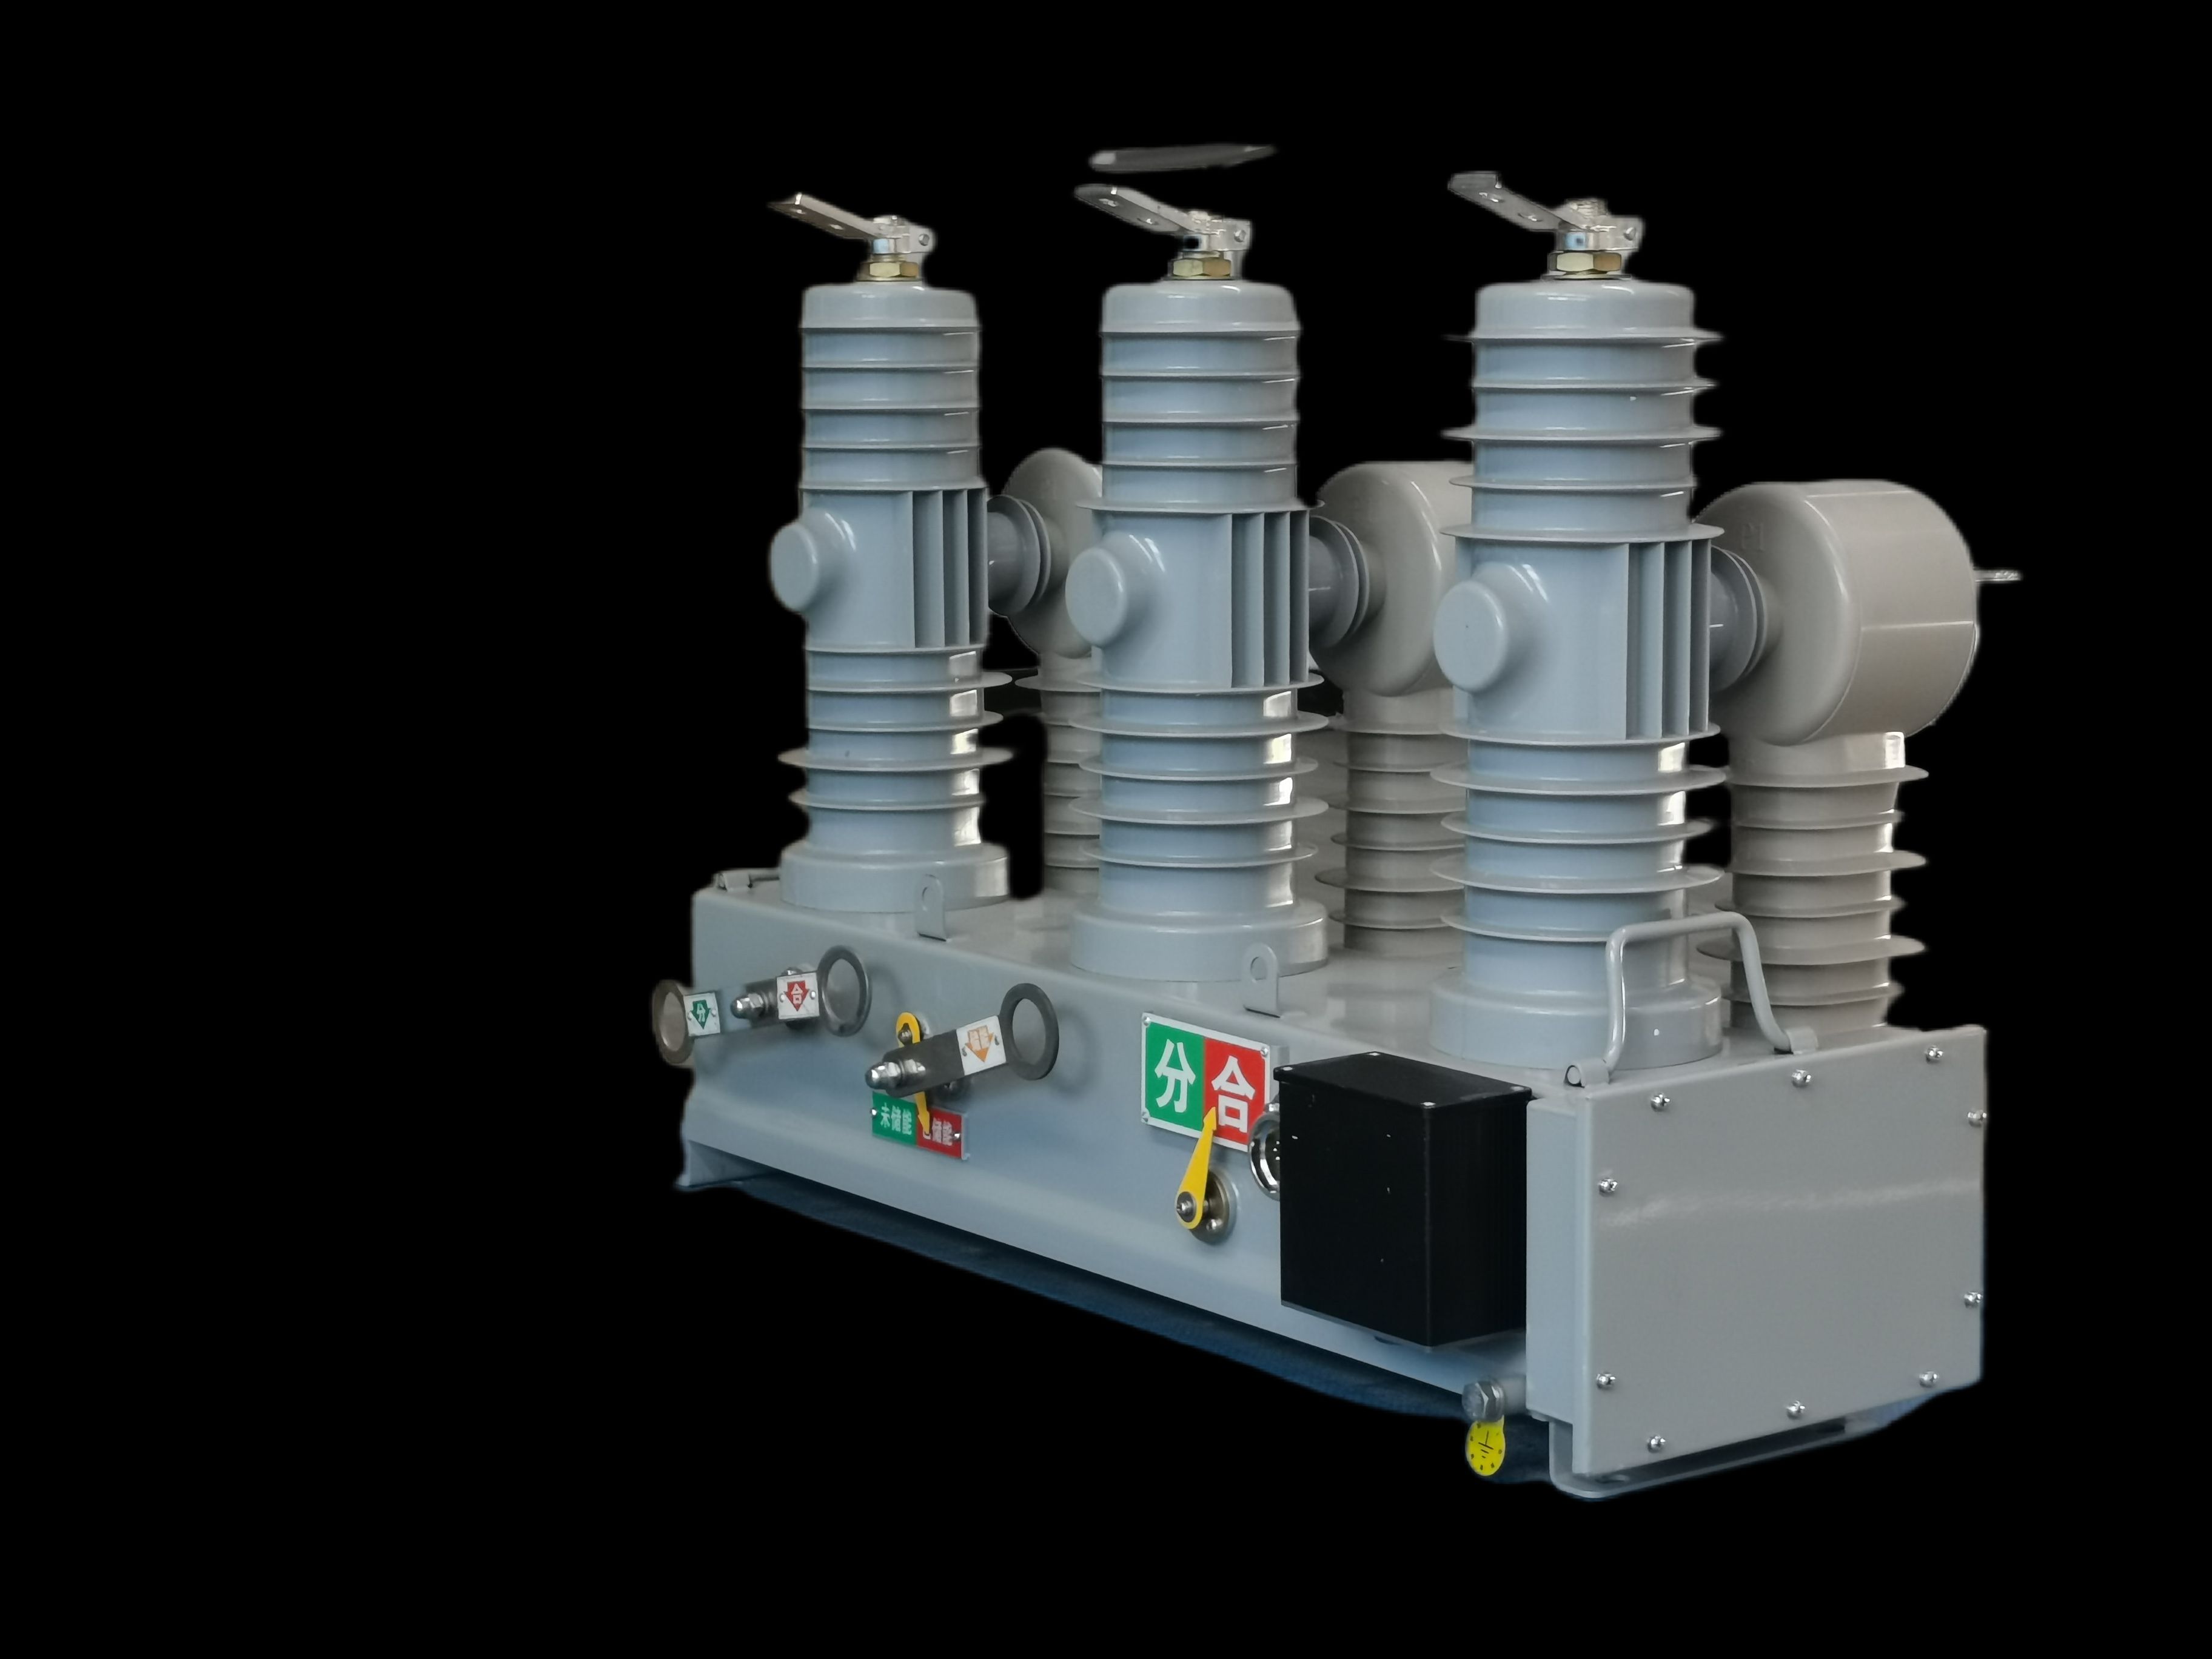
When a storm knocks out a distribution line at 3 a.m., the grid doesn't get a second chance—every millisecond of fault clearing matters. That's why Deepwill runs recloser production lines with the same discipline as a mission-critical assembly: automated precision, traceable components, and advanced testing that simulates years of field abuse. This post walks you through how those lines and test bays turn raw components into grid-hardened reclosers built for resilience.
Robotic Assembly Lines Built for Zero-Defect Reclosers
At the heart of the facility, each recloser moves through a sequence of robotic workcells where torque-controlled arms place contacts, operating springs, and vacuum interrupters with repeatable sub-millimeter accuracy. Every fastener is driven to a specific clamp load, and the data is logged against the unit's serial number before it leaves the station.
Inline inspection runs in parallel with assembly rather than after it. A mix of high-speed cameras and laser profilers scans each joint for micro-cracks, misalignment, or surface flaws, while force sensors confirm that moving parts glide without binding. If a measurement drifts outside its narrow band, the cell pauses and routes the unit to a containment area instead of letting the defect travel downstream.
Final validation is not a sampling exercise. Every completed recloser undergoes a full functional test under simulated fault conditions, including repeated open-close cycles at rated current and voltage. Only units that pass all electrical, mechanical, and thermal checks are released, giving utilities a device that can be installed straight from the crate with confidence.
Calibration Stations Where Every Millisecond Counts
Inside the narrow bay of an F1 garage, the calibration rig hums with the kind of tension you can feel in your teeth. A car rolls in after a hot lap, tires still radiating heat, and three engineers descend on the suspension pickup points. Every sensor they touch feeds a live data stream that refreshes every 0.2 seconds. The difference between a perfect toe angle and one that's slightly off won't show up as a red warning light—it'll show up three laps later as a tenth of a second lost through turn seven.
That same urgency plays out in semiconductor fabs, where lithography tools are recalibrated between wafer batches. A stage that drifts by a few nanometers can scatter a whole afternoon's yield. At these stations, millisecond-level timing isn't about speed for its own sake; it's about not letting a tiny drift compound into a costly rework queue.
The best calibration crews treat time as a raw material. They pre-stage torque wrenches, keep spare cables coiled in a specific direction, and rehearse handoffs until they're muscle memory. When the clock is running, no one asks what to do next. The only sound is the click of a connector seating home, and the soft beep that says the next measurement is already in tolerance.
Withstanding 40,000 Amps Before Leaving the Factory
Every unit gets slammed with a 40,000-amp fault before it earns a spot on the pallet. Not a simulated waveform on a laptop, but a real, full-scale short-circuit hit through the main contacts. The breaker has to interrupt that current, reset cleanly, and show zero damage to the arc chutes or the molded case. If it sounds like a thunderclap in the test bay, that's the point.
There's no sampling, no batch testing, no "representative unit" nonsense. Each serial number is bolted into the rig, hit with the full 40kA, then inspected under magnification for pitting, cracks, or heat discoloration. Thermal imaging records the case temperature during the event, and any unit that runs hotter than spec gets yanked from the line and torn down for root cause. The ones that pass feel almost bored by it, which is exactly what you want in a panel.
Inside the Climate Chambers That Mimic Coastal Corrosion
Stepping inside one of these chambers, the first thing you notice is the smell—warm brine and the faint tang of oxidizing metal. Racks of steel coupons, coated panels, and welded joints sit tilted at angles meant to catch every drift of salt fog. Nozzles hidden along the ceiling pulse a fine mist at intervals, while heaters and cooling coils chase each other through programmed cycles. It’s not just a salt spray booth; the room breathes, shifting from damp coastal dawn to scorching afternoon to cold, dew-heavy night in a matter of hours.
The real trick is in the rhythm. Some cycles drench the samples, then bake them dry until white salt crusts form in crevices. Ultraviolet lamps switch on to mimic sunlight breaking down polymer coatings. Then a condensation phase wets everything again without raining, the way fog settles on a pier at 5 a.m. Sensors track chloride deposition, surface wetness, and temperature gradients, feeding data back to a control system that adjusts the next cycle. What looks like random weathering is actually a tightly choreographed assault on every weak point in the material.
Engineers use these chambers to compress years of coastal exposure into weeks or months. A new alloy might survive 2,000 hours in the chamber and still crack near a weld in the field, so the results are always cross-checked against outdoor test sites in places like Kure Beach or the North Sea. Still, the chamber gives a first read on whether a coating will blister, a fastener will pit, or a galvanic couple will eat itself alive. It’s not a perfect stand-in for the ocean, but it’s close enough to kill a bad design before it ever touches salt water.
Fault Injection Rigs That Rehearse Real Grid Collapses
In a dimly lit warehouse outside Knoxville, a team of engineers gathers around a steel-encased transformer that hums with simulated load. They are not waiting for a storm or a cyberattack; they are scripting one. Using a fault injection rig, they deliberately short a relay, spike a voltage regulator, and corrupt a sensor reading just to watch how the local grid segment buckles and recovers. It is chaos by design, a full-scale rehearsal of failures that most utilities hope never to see outside a lab.
These rigs are essentially time machines for grid operators, letting them compress decades of rare but catastrophic events into an afternoon. Instead of relying on paper studies or half-remembered anecdotes from the last blackout, technicians can induce a phase-to-phase fault on a feeder, then measure exactly how long it takes for a recloser to lock out or for a distributed energy resource to island itself unintentionally. The data is ugly and beautiful: breaker trip curves that drift from spec, protective relays that mis-coordinate under harmonic distortion, and control room alarms that cascade in ways no one predicted.
What makes the modern fault injection rig stand out is its ability to weave together physical hardware and virtual grid models. A controller can inject a synthetic frequency excursion into a real inverter while simultaneously feeding a false SCADA status to the operator's console. The result is a rehearsal so convincing that trainees sometimes forget it is not a real collapse until the rig resets and the lights stay on. That realism is the point: better to rehearse a collapse a hundred times on a test bench than to meet it once, unscripted, on a live network.
Traceability Protocols That Follow Each Recloser for Decades
Every recloser leaves the plant with a unique identifier that stays attached through substation moves, utility acquisitions, and decades of maintenance work. That identifier is not just a stamped serial number. It links into a living file where test reports, firmware revisions, field repairs, and even weather-related stress events accumulate over time. Because a recloser can easily stay in service for twenty or thirty years, the traceability protocol has to survive staff turnover, software platform changes, and record-keeping migrations without dropping the thread.
The real payoff shows up when a unit from the early 2000s comes back for refurbishment. Instead of puzzling over its past, a technician can pull the complete chain of custody: original acceptance tests, every fault interruption logged by the controller, replacement notes for bushings or vacuum interrupters, and firmware patches applied after commissioning. That depth of history changes the conversation from guesswork to a precise understanding of what the unit has endured and what it still requires before going back into service.
Maintaining that trail for decades means the protocol cannot depend on a single person's memory or a binder in a back office. It normally combines physical tags rated for outdoor exposure, database fields that remain stable across system upgrades, and periodic audits that catch missing entries while the recloser is still running. When the protocol works, nobody thinks about it until the day it prevents a utility from scrapping a perfectly good unit or from missing a critical safety retrofit.
FAQ
They rely on semi-automated workstations that combine robotic placement with manual torque verification, ensuring each interrupter is seated within micron-level tolerances before the next stage.
Beyond routine dielectric and contact-resistance checks, production batches undergo simulated fault interruption, temperature-rise runs at rated current, and mechanical endurance cycling that mimics years of field operation in a matter of days.
Factory testing catches latent defects—such as gas leaks, misaligned actuators, or timing drift—under controlled conditions, so utilities receive units that behave predictably during storms and overload events instead of discovering issues during an outage.
Automated calibration sequences adjust trip curves and protection settings to the exact specification of each utility order, logging every parameter so traceability is maintained from raw component to final crate.
Modular assembly cells allow quick changeover between 15 kV, 27 kV, and 38 kV models, while a dedicated test bay reconfigures its load banks and relay interfaces to match the control scheme being shipped.
Finished units are placed in thermal chambers that cycle from -40°C to +65°C, followed by salt-fog exposure and rain testing under voltage, verifying that seals and electronics survive coastal, desert, and arctic installations.
Each mechanism is driven through 10,000 open-close operations while sensors monitor travel, velocity, and damping; any deviation beyond preset limits triggers automatic rejection and root-cause analysis before the unit can proceed.
Conclusion
At the heart of modern recloser manufacturing, robotic assembly lines have shifted the goal from simple throughput to a stubborn pursuit of zero defects. Every contact, coil, and actuator is placed with repeatable precision, while inline vision systems and torque monitoring catch deviations that human eyes would miss. Just downstream, calibration stations treat timing as a life-or-death specification. Technicians and automated benches verify that trip curves and reclosing intervals align within milliseconds, because on a live feeder, a sluggish response can turn a branch fault into a neighborhood outage. These stations do not merely confirm settings; they force each unit to prove its sense of urgency again and again.
Before a recloser earns its nameplate, it faces a battery of tests meant to mimic the worst the grid can deliver. Short-circuit cells push 40,000 amps through the interrupter to confirm it can clear and reclose without mechanical distress. Climate chambers then cycle temperature and humidity while spraying salt fog, reproducing years of coastal corrosion in compressed time. Fault injection rigs go further, staging artificial line-to-ground and line-to-line collapses so the relay behaves exactly as it would during a storm or fallen tree. Finally, traceability protocols assign each unit a digital birth certificate, recording materials, test results, and calibration data so that decades later, a utility engineer can pull up the full history before a single truck rolls.
Contact Us
Contact Person: Julion
Email: [email protected]
Tel/WhatsApp: 8617351370631
Website: https://www.deyunelectric.com